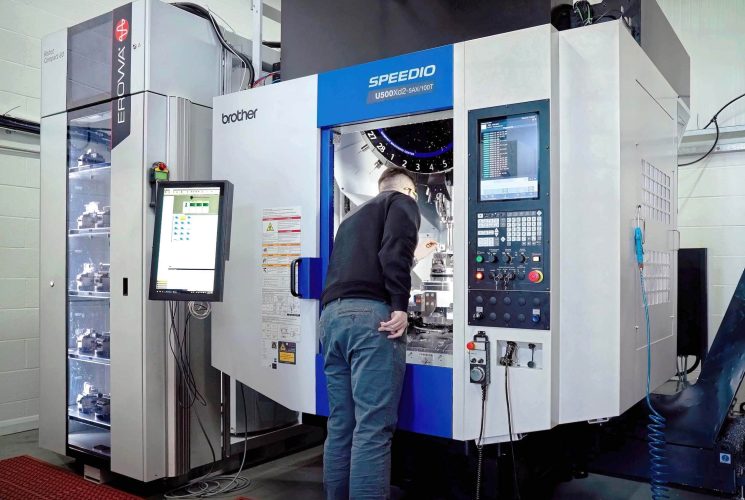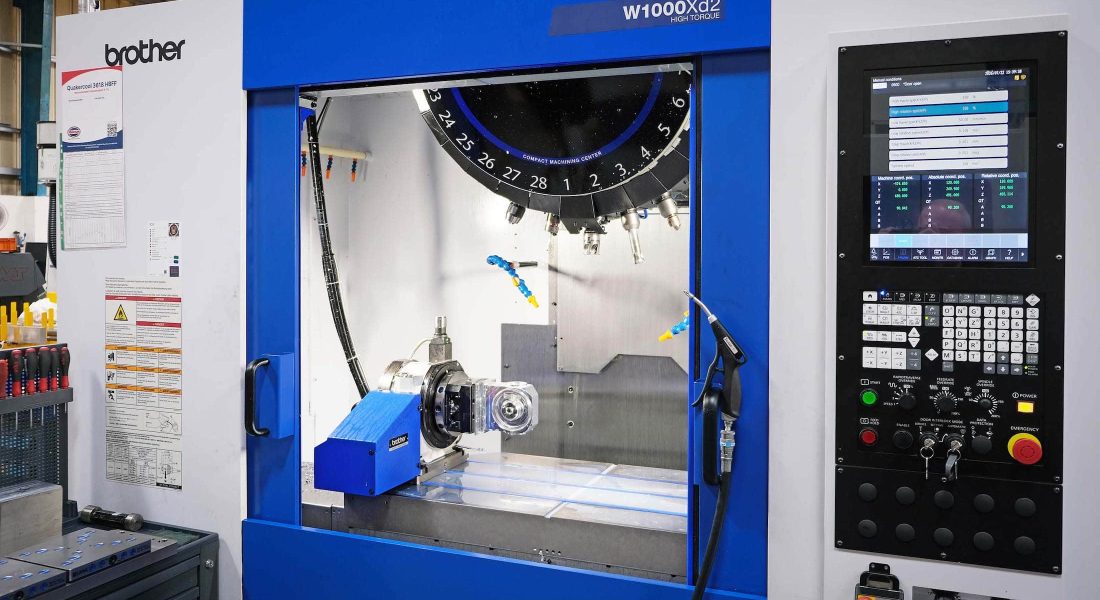
Subcontractor Diamond Precision Engineering (DPE), which has used three 40-taper vertical machining centres (VMCs) and a BT50 model for many years, has for the first time opted to invest in a 30-taper machine. It is a Japanese-built Brother Speedio W1000Xd2 with a dual-contact spindle-to-toolholder interface, a style of BBT30 machine that DPE director Harry Pitt regards as the future of series production.
Installed at the end of last year (2025) by Brother’s sole UK and Ireland agent Whitehouse Machine Tools, the machine benefits from a BIG-PLUS face-and-taper spindle that is also high-torque, rated at up to 92 Nm. The combination allows tough materials like titanium, Inconel and stainless steels to be machined productively and accurately, provided that optimised cycles are employed.
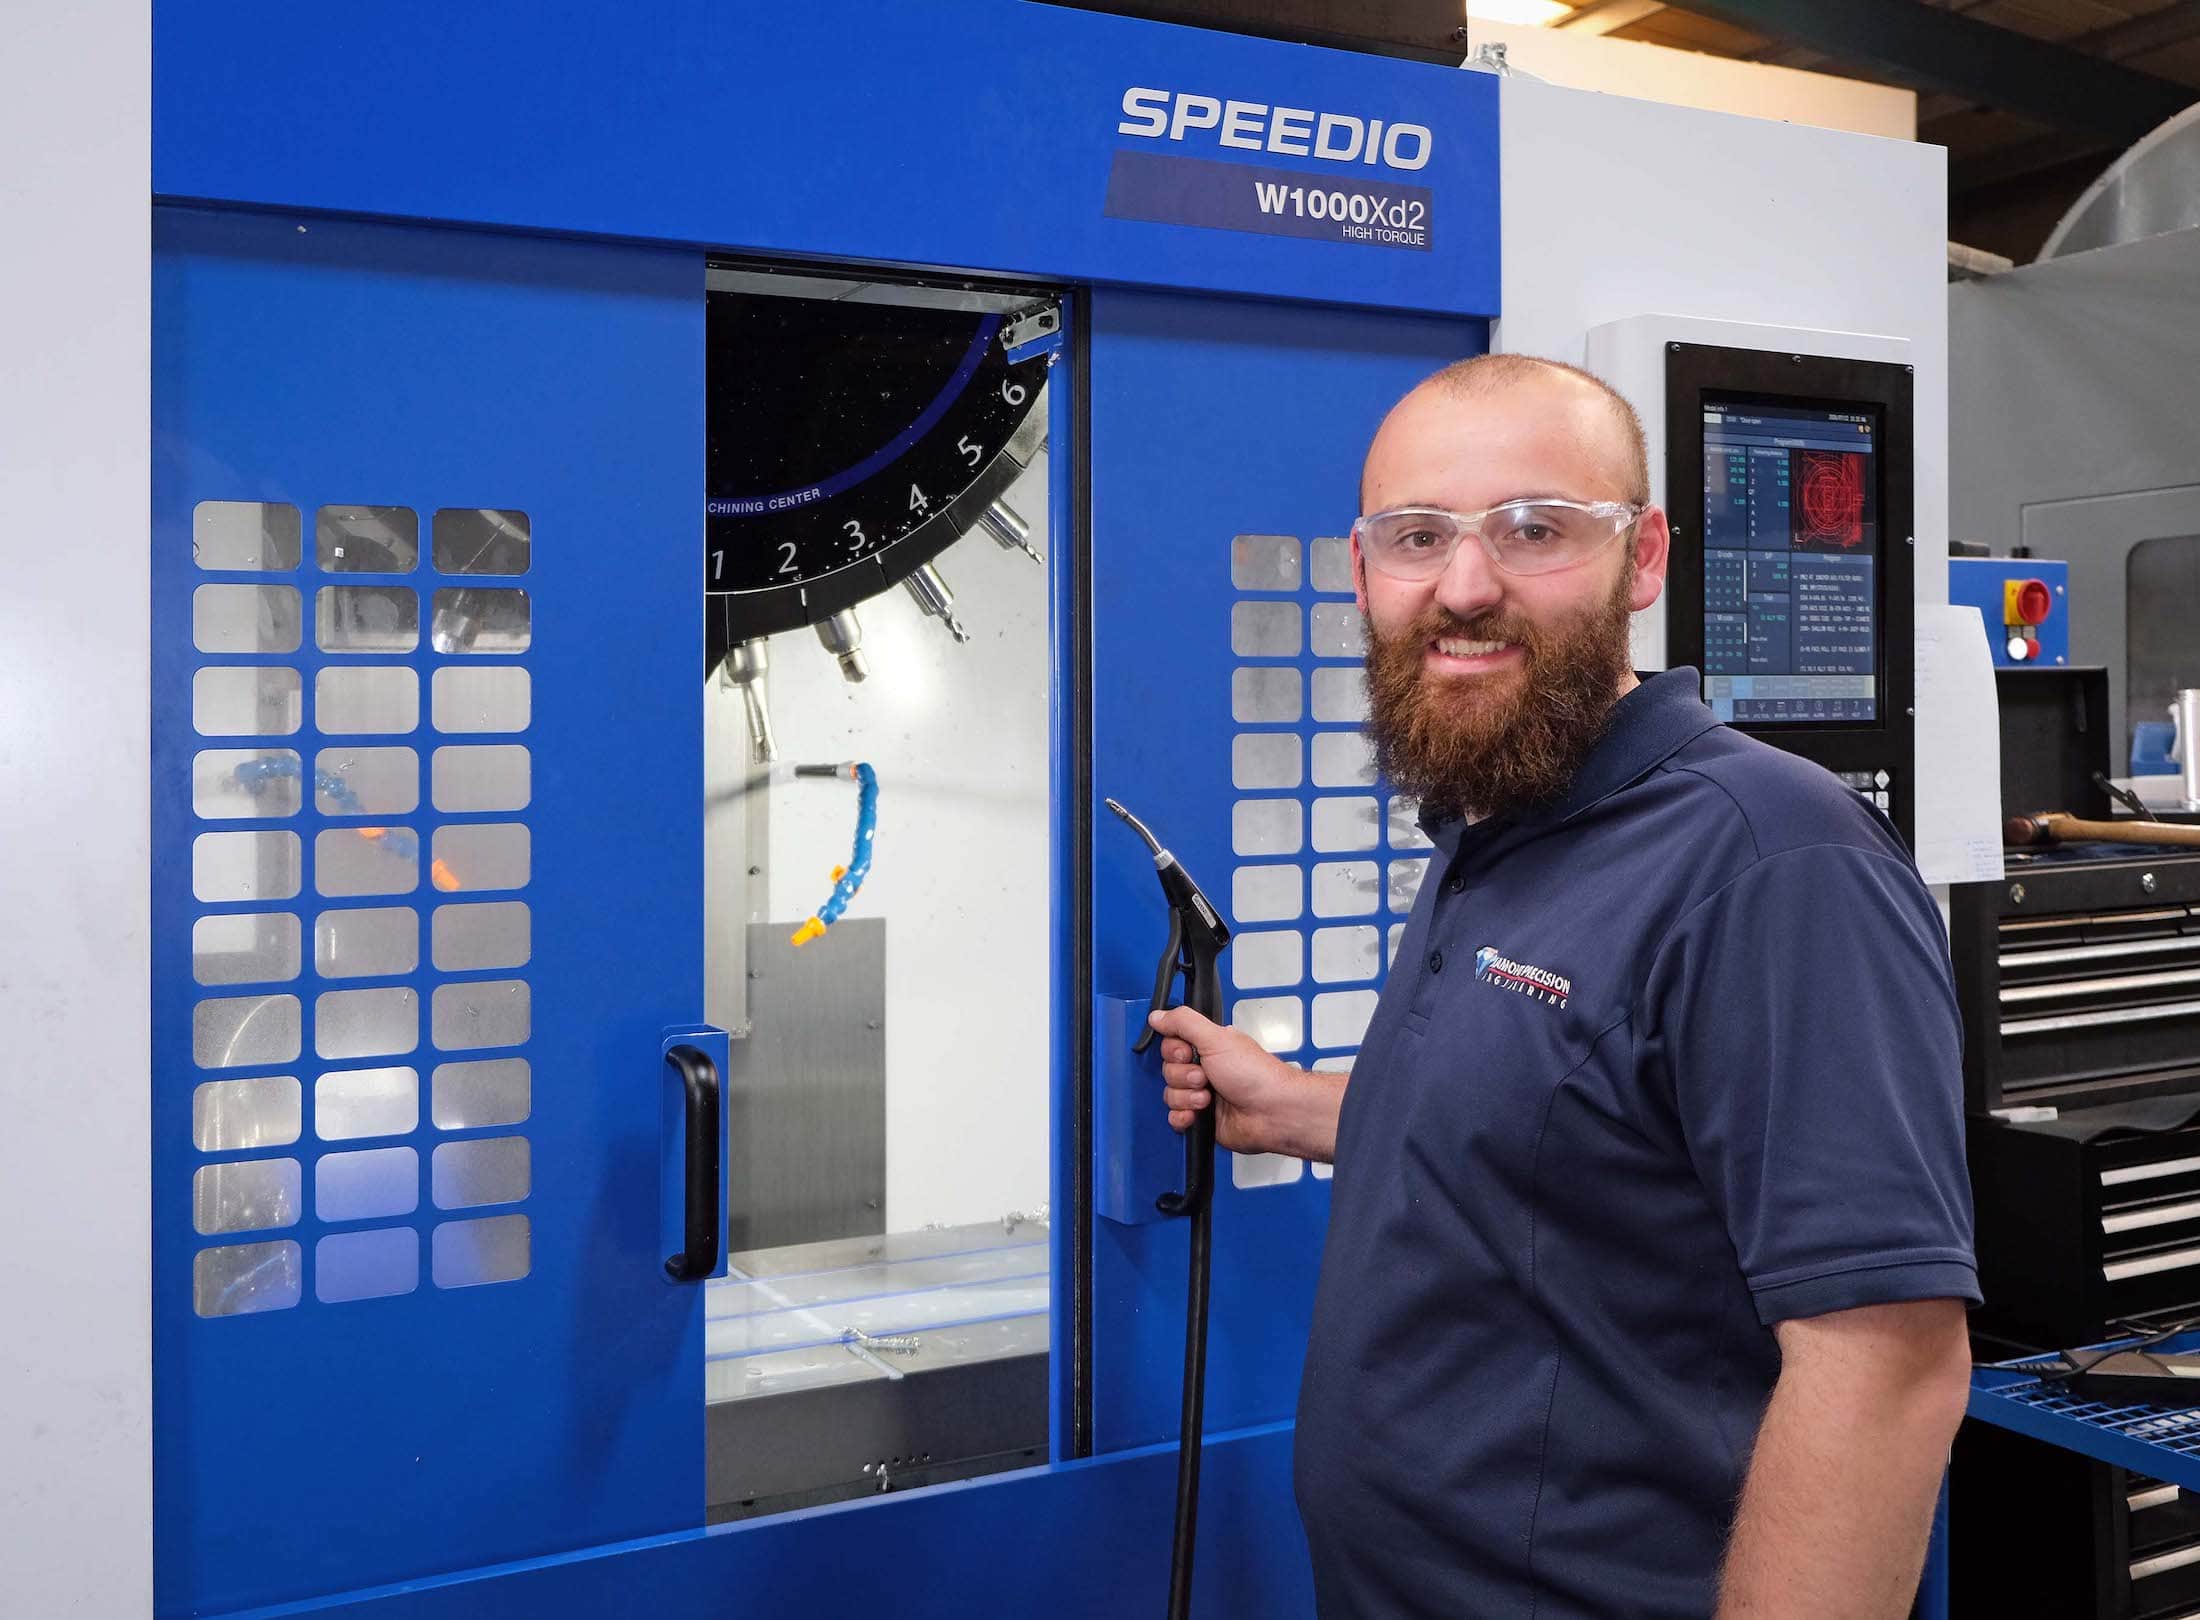

DPE was established in 1986 by Harry’s father Graham. It comprises a separate laser cutting and fabrication facility run by another of his sons, Oliver, who provides 20% of the milling, drilling and grinding work taken on by Harry’s machining division in Kelvin Park, Birkenhead, which opened in 1996.
There are now five CNC VMCs in use plus four manual mills and a similar number of lathes, work being split roughly 50:50 between rotational turn-milling and prismatic machining. The rail industry accounts for about half of turnover, while stainless steel pumps make up a further 20%. The remainder of contracts is split across diverse sectors, with supply of fixtures to automotive and aerospace manufacturers a major activity.
Harry describes the Brother Speedio’s productivity and ability to make DPE money as “immense” and it was the main reason he decided to go down the BBT30 route. He is unconcerned that the latter taper is a little over a quarter smaller in diameter at the gauge line and across the flange compared with a BT40 interface. That is because his selection of the dual-contact, high-torque spindle variant of the W1000Xd2 gives him equivalent strength and rigidity.
Both Harry and Oliver are keen cyclists and were impressed to see the lines of Brother and other high-speed machine tools in operation at the Barnoldswick factory of mountain bike aftermarket components manufacturer, Hope Technology. Successful cutting trials on several DPE parts were carried out at Whitehouse Machine Tools’ technical centre in Kenilworth, after which the decision to purchase the Brother Speedio was made.
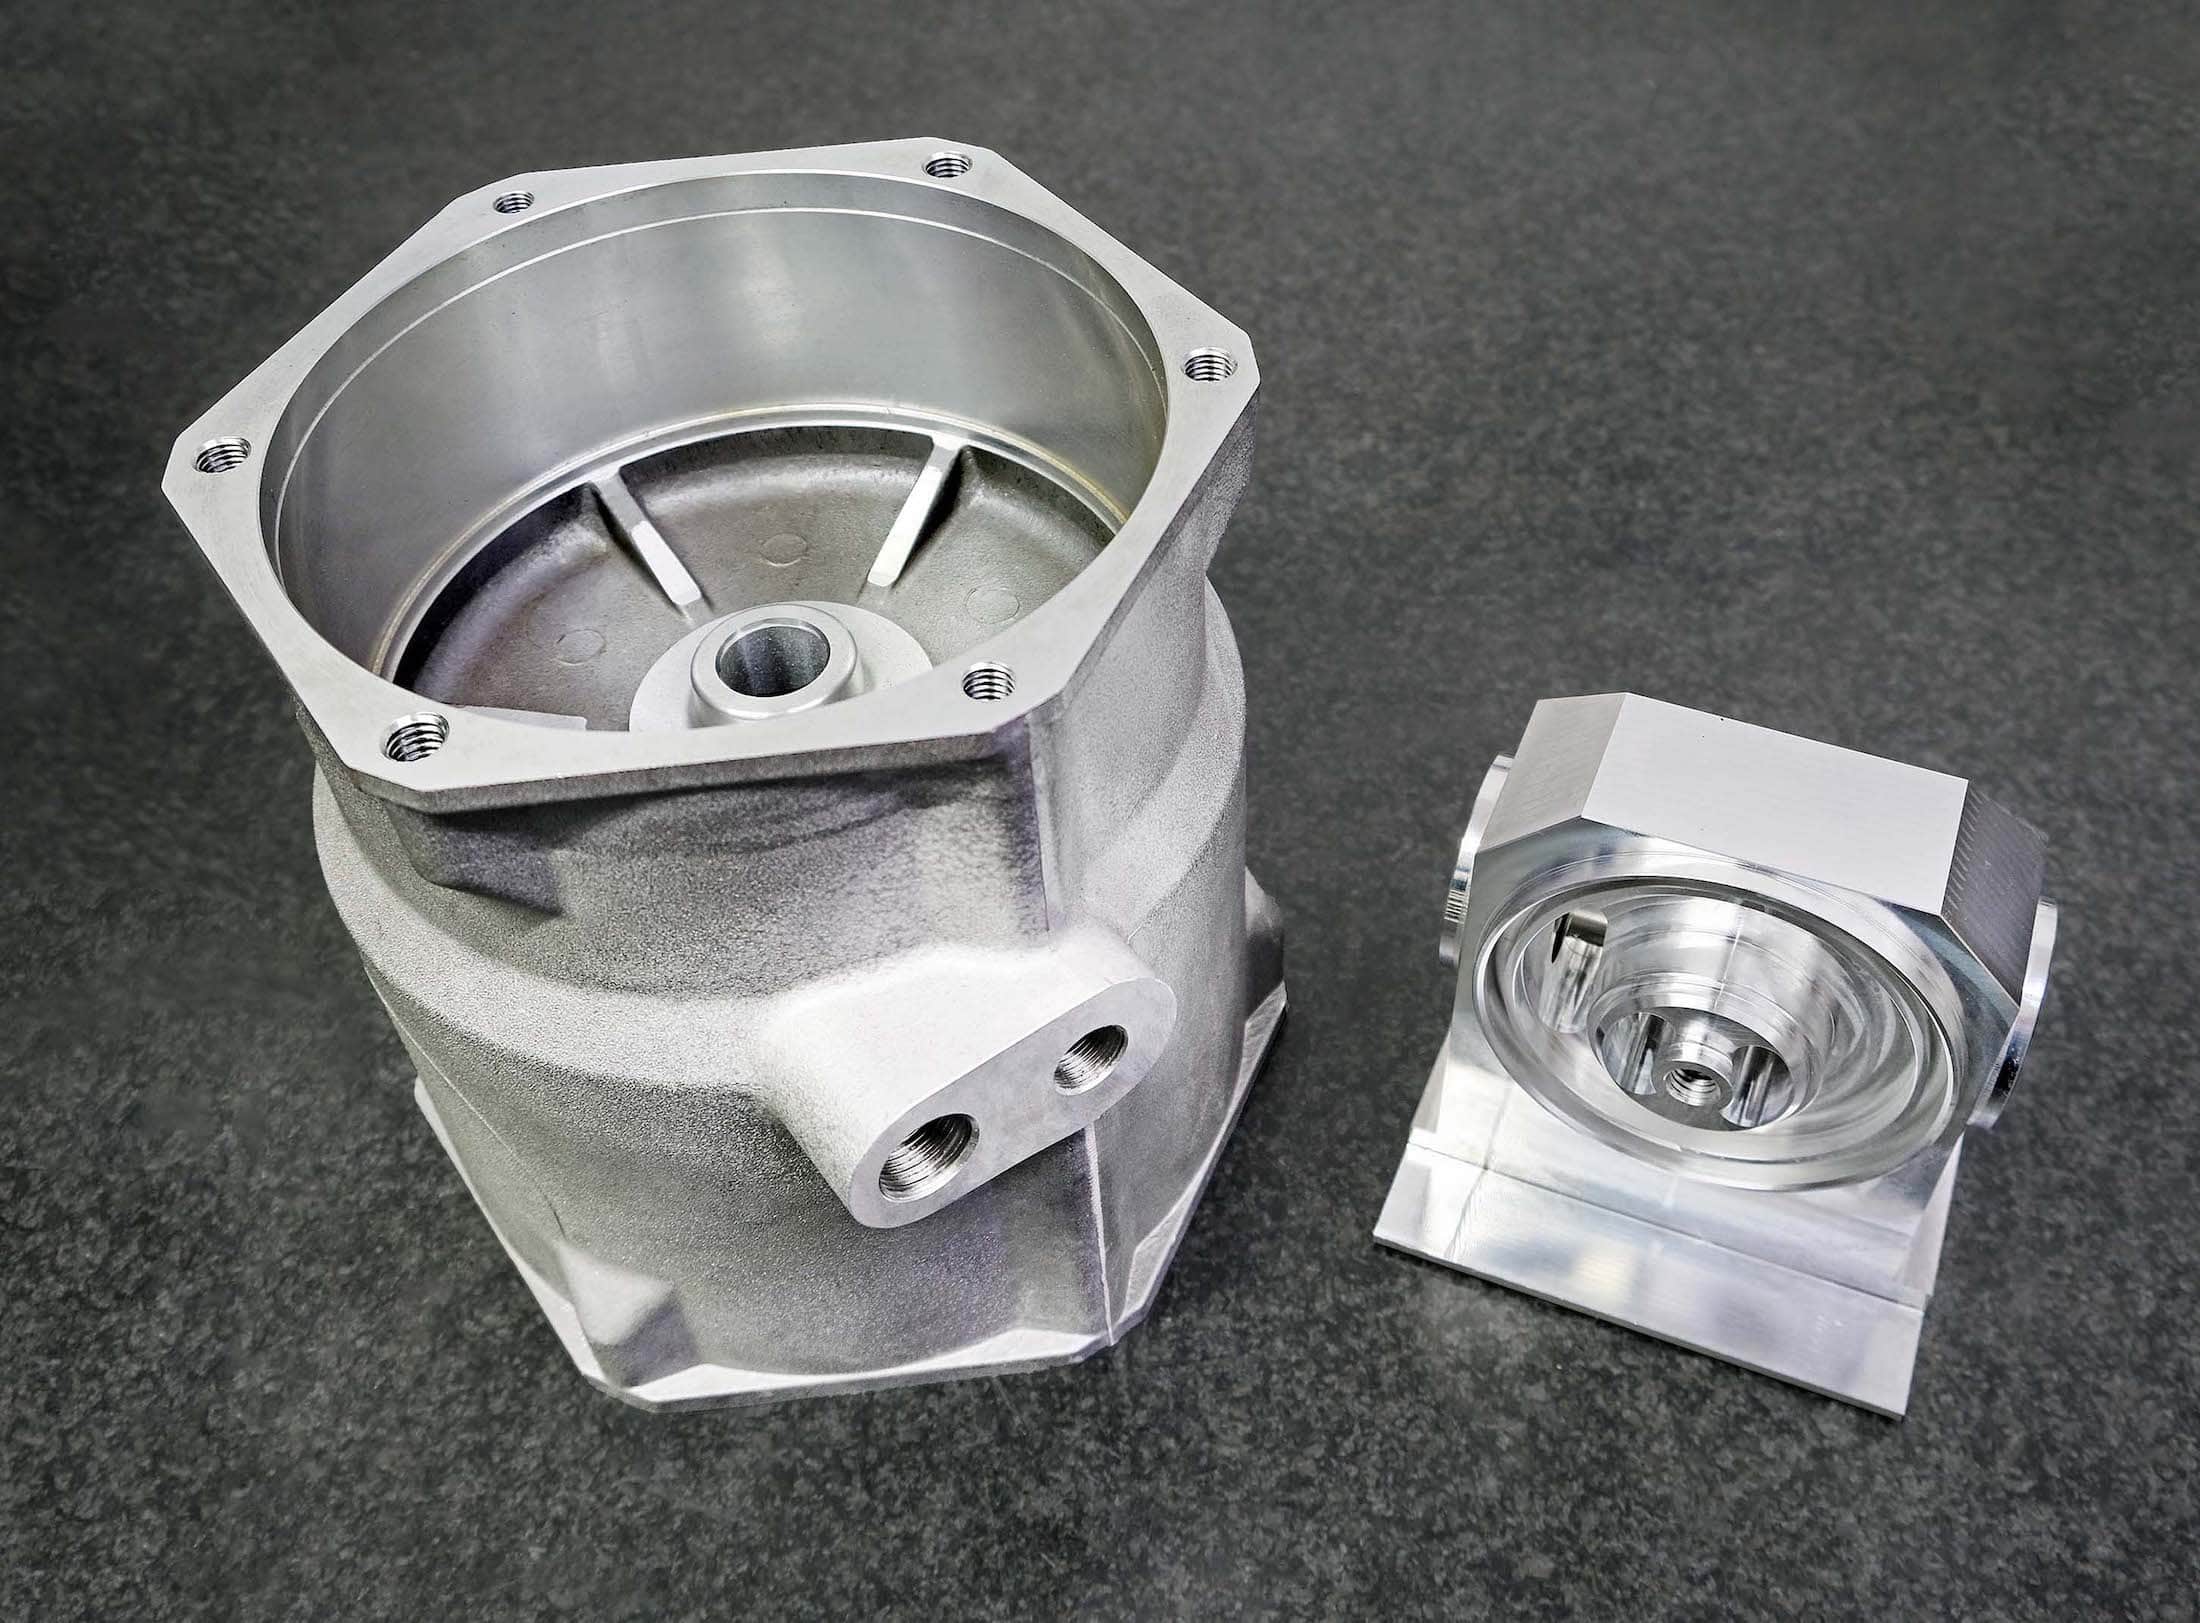
During the first six months of operation in Birkenhead, approximately 10 parts were transferred from BT40 VMCs to the 30-taper machine, with impressive results. General machining tolerance held is ±0.05 mm, although sometimes it can be much tighter.
In one instance, a mild steel automotive component’s cycle time fell from five to three minutes, a 40% reduction. In this case the programmed feeds and speeds were kept the same as on the BT40 machine. So the time saving was purely a result of shorter idle times on the Brother Speedio due to 50/50/56 m/min rapids in X/Y/Z, 1.4 seconds ATC chip-to-chip, and 0.15 seconds start/stop time to and from the maximum spindle speed of 10,000 rpm.
The cycle involved some rigorous cutting with a 12 mm solid carbide end mill, confirming the robustness of the W1000Xd2, with its vibration-damped, FEA-optimised, heavily ribbed cast iron frame. As 500 of the components had been ordered, by the time they were delivered nearly 17 hours of machining time had been saved.
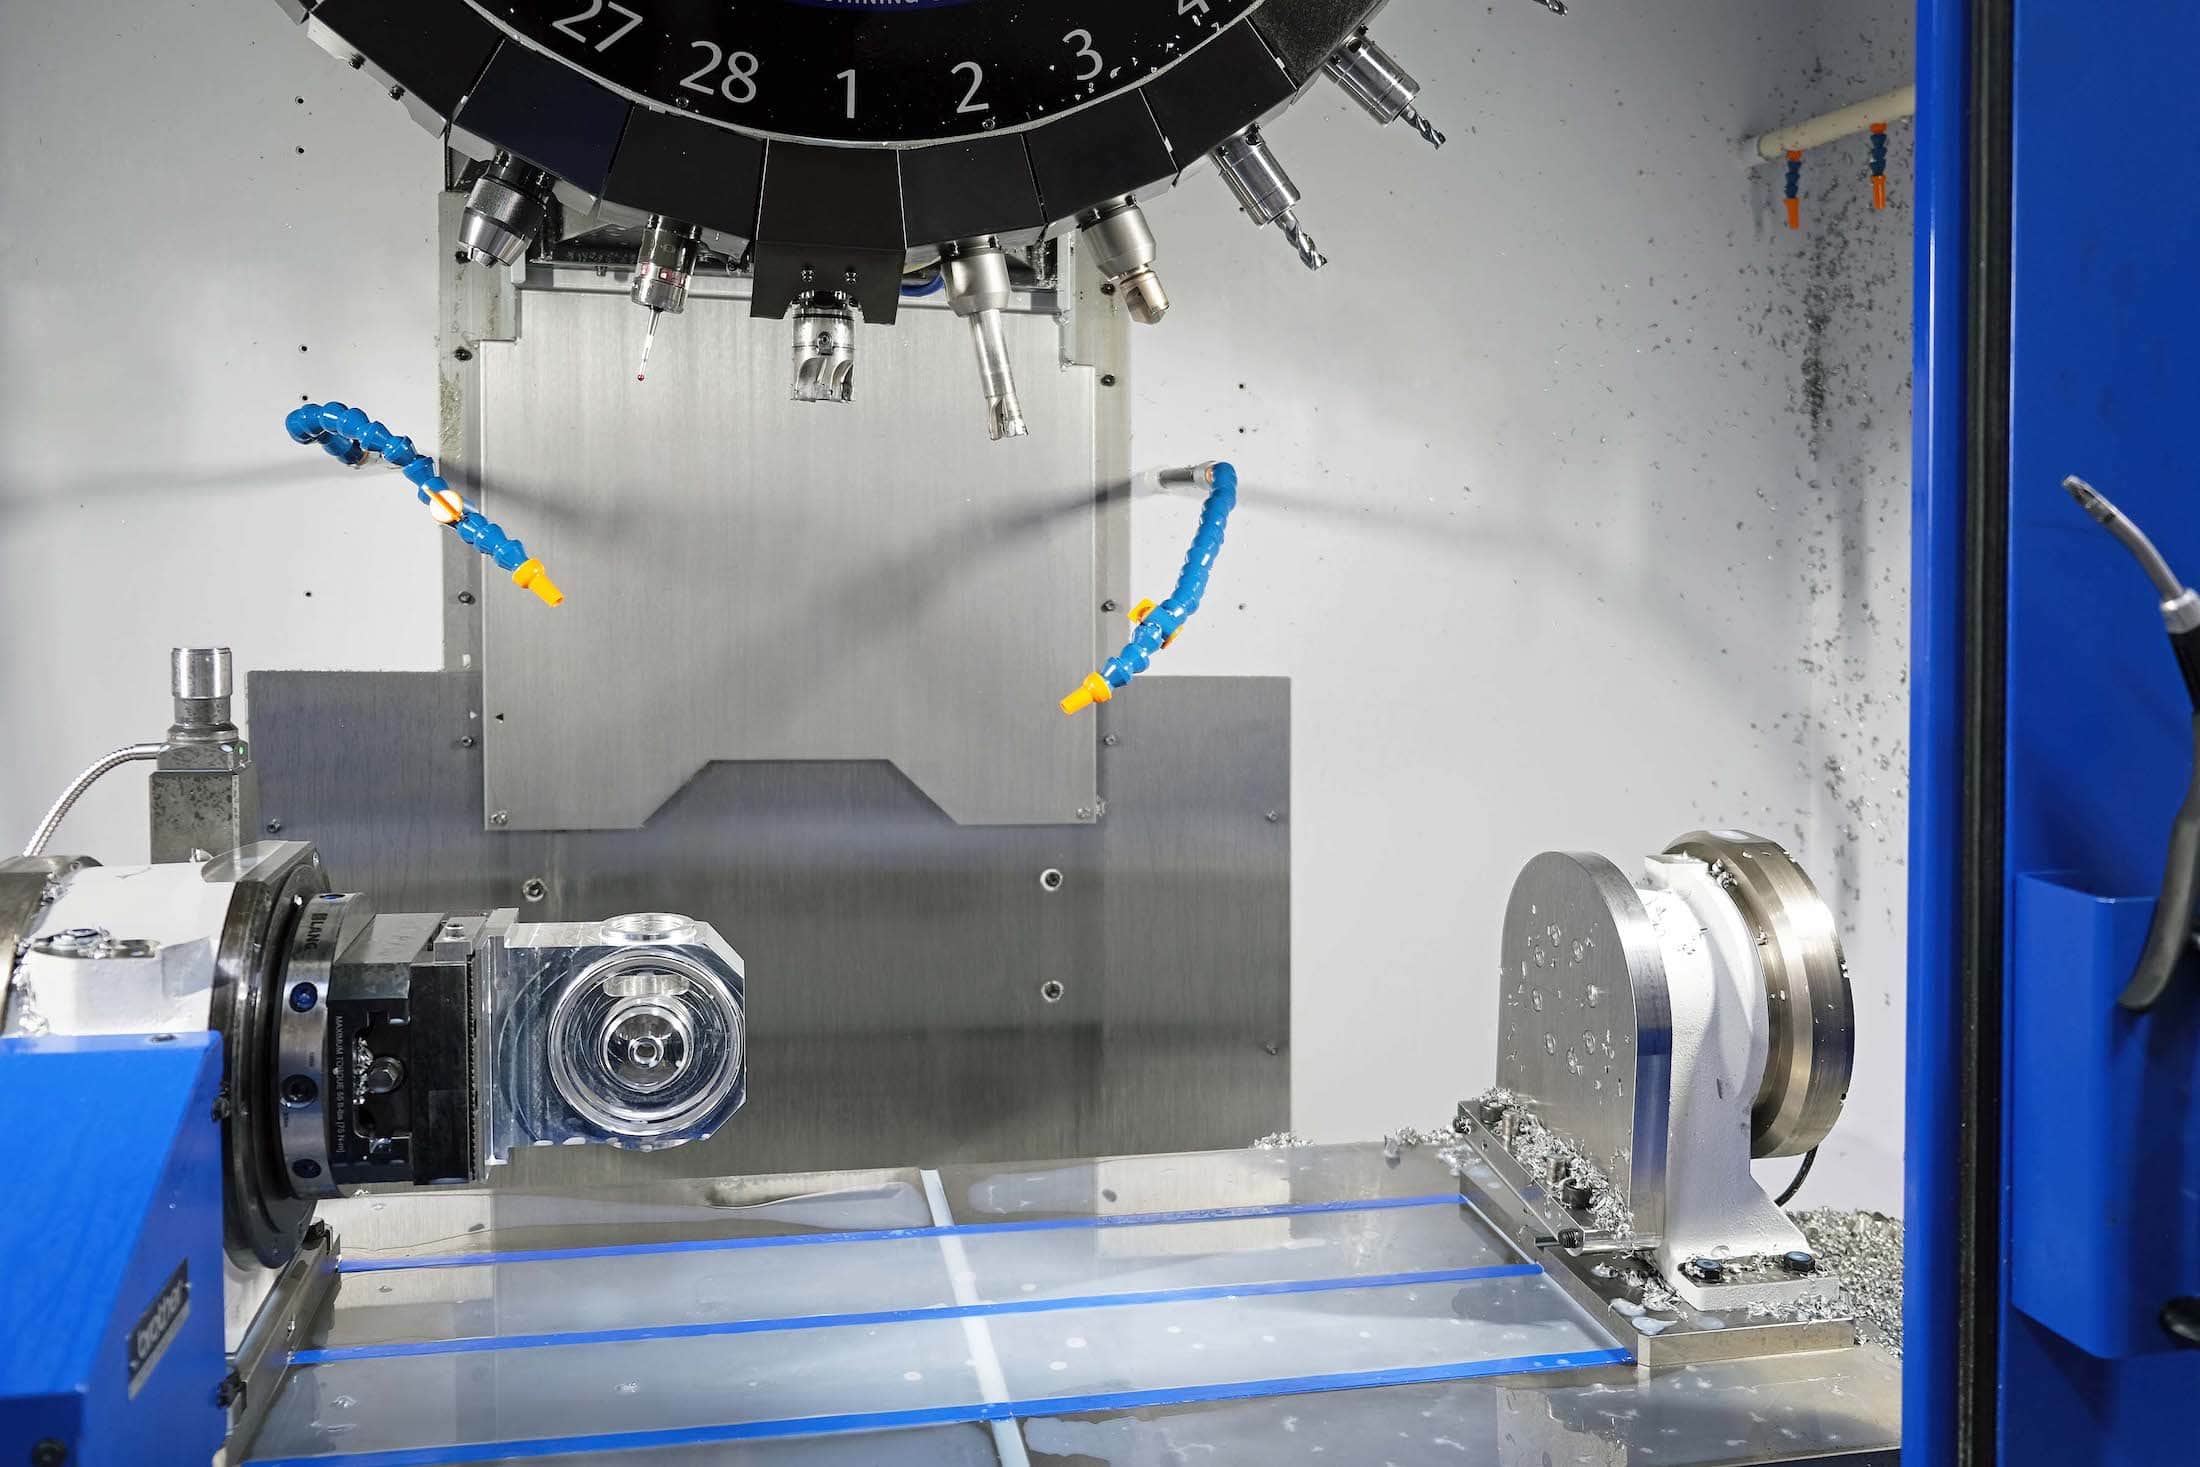
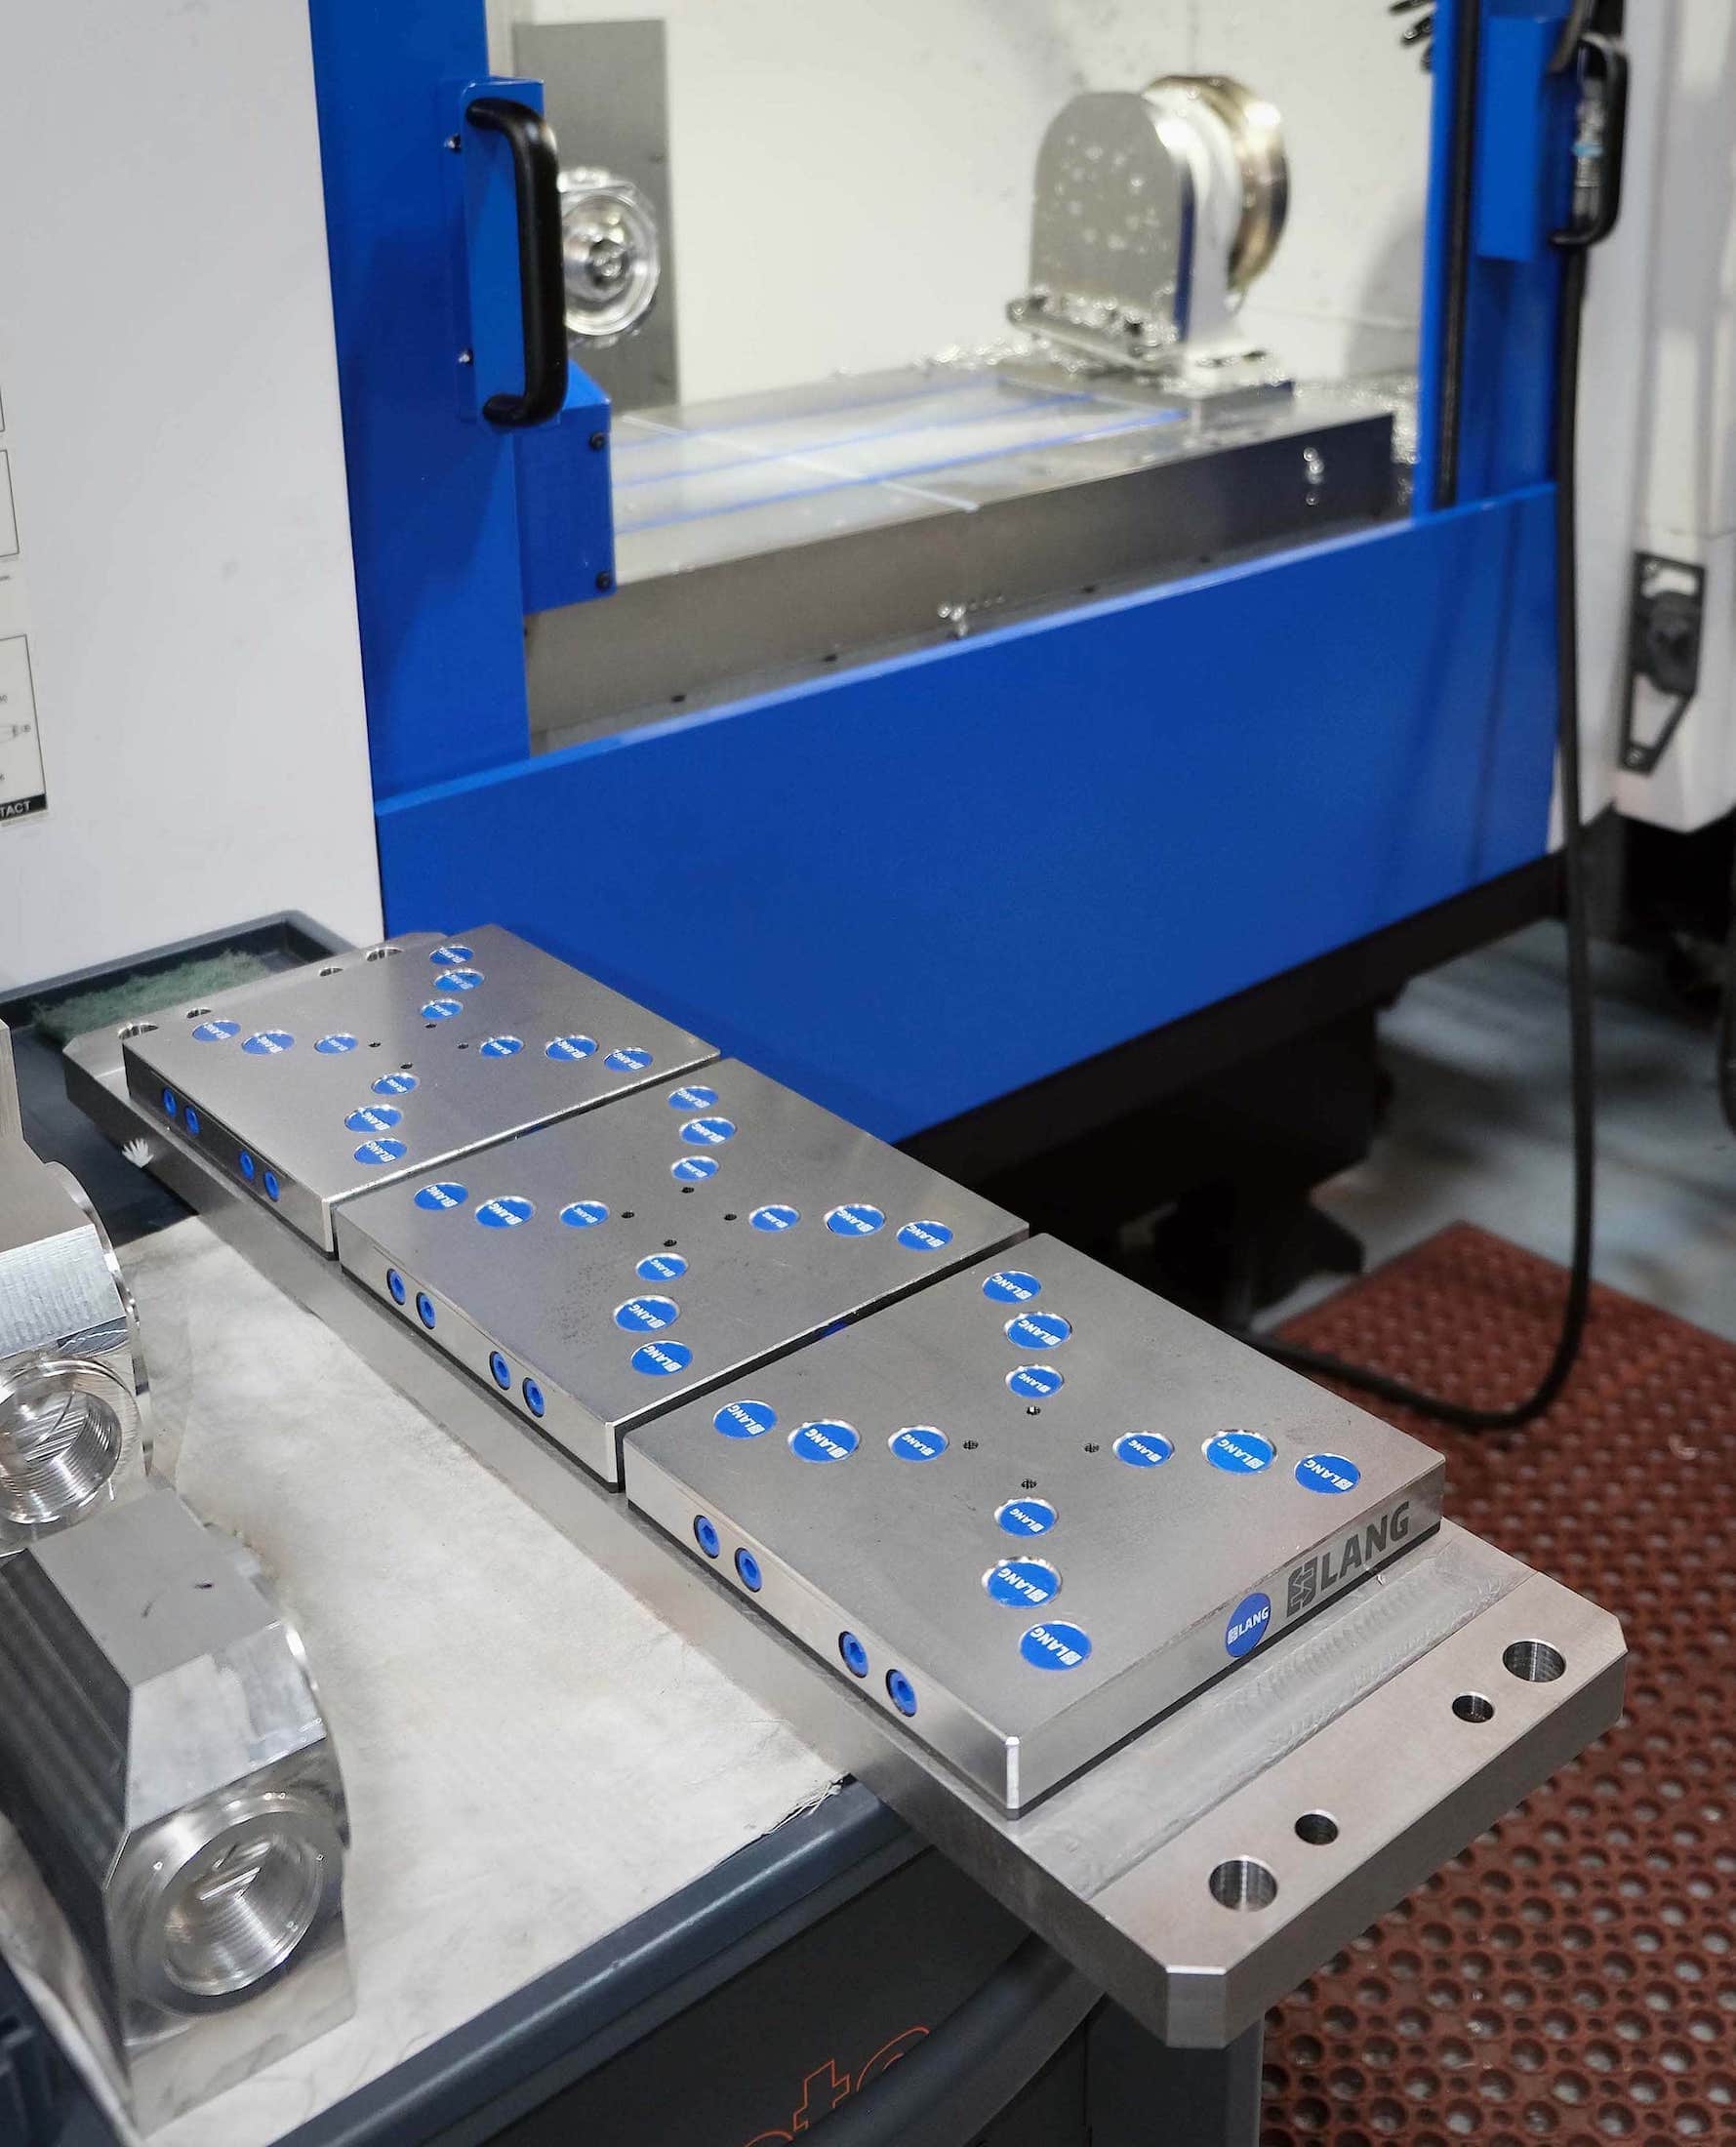
Another example cited was the transfer of stainless steel pump parts, which were mounted 10 at a time on a double-sided trunnion equipped with Lang workholding plates, rotated by a CNC indexing head secured to the 1,100 mm x 500 mm machine table. The component required a hole to be produced with a 30 mm solid carbide drill and the program included a lot of repositioning for drilling further holes. The cycle time for this component was cut substantially and a large batch of them was required, leading to a significant production cost saving.
Thirdly, an aluminium casting for the rail industry was transferred because, by mounting two of them on the swivelling trunnion, it can be completely machined in Ops 1 and 2 so that a part comes off the machine complete every time the Brother Speedio’s doors open. Previously a third operation was required, entailing another setup.
A final example mentioned by Harry was the production from a solid aluminium billet of an aerospace component. For this, the trunnion was removed and the billet edge milled with a tapered slot for clamping on 3 mm of material in a Lang dovetail vice mounted directly onto the indexing head. Although edge preparation for clamping took extra time, what were previously four machining operations were condensed into one, after which a further operation was completed on a BT40 VMC to free up the faster machine to start the next part.
Cycle time on the Brother Speedio is 24 minutes, compared with the considerably longer time previously required for the four operations it has taken over. A great deal of setup and handling time has been eliminated in addition. Harry confirmed that the job is now profitable, whereas before it was very difficult to make money on it.
He added that he is impressed with the quality of the Brother Speedio’s build and the attention to detail in its construction. For instance, when removing panels, the use of self-retaining screws ensures that they do not disappear into the machine, never to be seen again. The Brother grease system for lubricating the slideways is a benefit, as oil does not contaminate the coolant, which in practice means he never has to switch the skimmer on.
Another elementary feature he likes is that both doors open as one or other handle is pulled back, an unusual feature in manual operation. It is only a small thing, but nevertheless something the operator has to do numerous times every day and shows the thought that has gone into the machine design.
In addition to the BBT-specification spindle, another non-standard facet of the installation is an extra-wide swarf conveyor and bin, commensurate with the high metal removal rate of the W1000Xd2. It ensures, for example, that the operator does not have to keep stopping the machine to empty a standard bin containing voluminous amounts of aluminium swarf, or even of mild steel chips generated when machining rollercoaster parts requiring a lot of metal removal.
The machine has high pressure coolant delivery, including through the spindle, for efficient swarf management. As the swarf conveyor is solid rather than slatted, a lot of coolant ends up at the bottom of the swarf bin. So a Woogard closed-loop recirculation system has been fitted to return it to the coolant tank, conserving a consumable that is becoming increasingly expensive.
Regarding the service he has received from Whitehouse Machine Tools, Harry cannot praise it too highly, from communication with the company at the outset, to ongoing attentiveness to queries throughout the purchasing process, to machine delivery and commissioning, and on to training. He is confident that this will be mirrored by the supplier’s service backup.
He was delighted when he gained unexpected business from an E-bike manufacturer that was going to buy a Brother Speedio but has not yet done so. Whitehouse mentioned to Harry that the company wanted its parts made on this type of 30-taper machining platform, so some of this extra business has already ended up in Birkenhead, with more to follow.